Quality and certificates
Our management system is certified to ISO 9001, ISO 14001 and ISO 45001. Factory production control is certified to EN 1090 for structural components up to EXC3, and welding to EN ISO 3834-2.
- Audited by
- TÜV Rheinland Bulgaria and TÜV Rheinland Polska
- ISO 9001
- Certified since 08.07.2005
- EN 1090
- Structural components up to EXC3
- Welding
- EN ISO 3834-2, valid to 04.11.2029
- PED
- Module G, item by item
Verify our ISO and EN ISO 3834-2 certificates on TÜV Rheinland Certipedia (opens in a new tab) ID 9105031549
Certificates
Select a certificate to see it at full size with its number, issuing body, validity and scope.
Registrations in Bulgaria
State Agency for Metrological and Technical Supervision
Registered for maintenance, repair and reconstruction of boilers, pressure vessels, steam, hot-water, oil and gas pipelines, gas and LPG installations and lifting equipment.
Central Professional Register of the Builder
Entered for buildings, energy and utility infrastructure, and construction and installation works.
Documentation for each order
With each order we hand over a QA dossier and the welding records for that order.
Typical QA dossier
The content of the dossier varies according to the client's requirements.
- Inspection and test plan (ITP)Agreed before fabrication starts, with your hold and witness points
- WPS, PQR and welder qualificationsWelding coordinated under EN ISO 3834-2
- Material certificates and traceabilityFull material traceability, as on the furnace combustion chamber for a district heating plant in North Macedonia
- NDT, dimensional and coating reportsSigned off against the agreed acceptance criteria
- DoP, DoC and CE markingAs-built documentation at handover
Welding
Our welding coordinator is qualified IWE/IWI and keeps the list of qualified welding procedures.
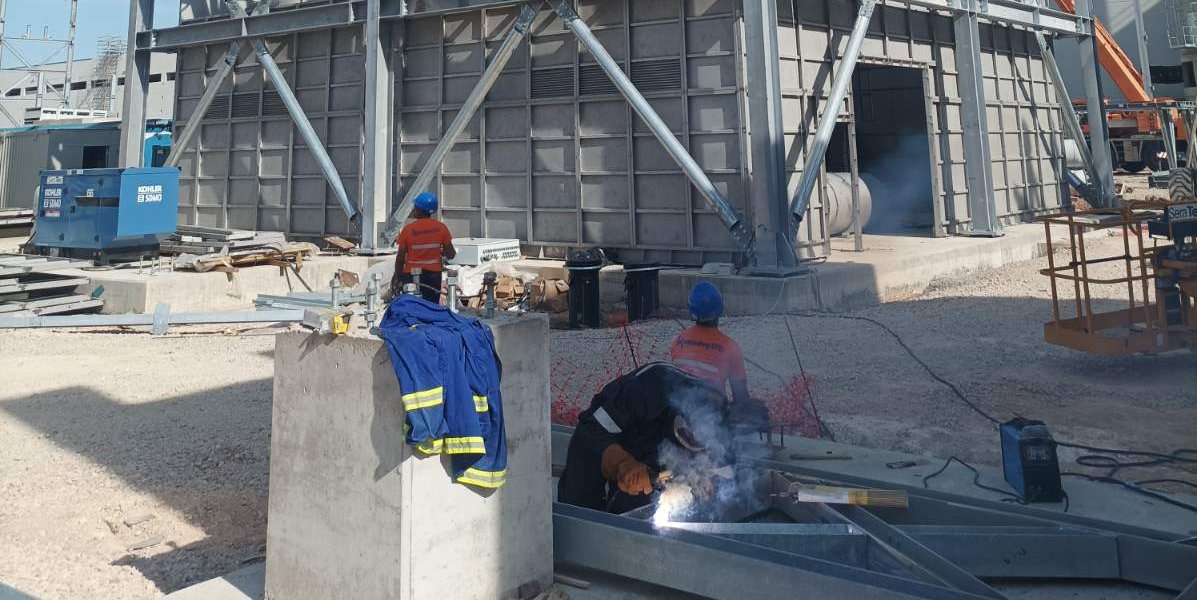
Welding to EN ISO 3834-2
- Standard
- EN ISO 3834-2, comprehensive quality requirements
- Processes
- MMA, MAG and TIG
- Stations
- 21 for MIG/MAG, TIG and MMA, plus an orbital pipe welder up to Ø 610 mm
Coordination and qualifications
- Coordination
- Responsible welding coordinator qualified IWE/IWI
- Procedures
- 25 qualified welding procedures (list of 02/2024), most witnessed by TÜV Rheinland Bulgaria
- Range
- Plate, pipe butt, branch and pipe-to-plate joints, including stainless to carbon steel; thicknesses up to 50 mm
- Welders
- Qualified by notified bodies under PED; each qualification is confirmed every 6 months
Inspection and testing
Inspection follows the inspection and test plan (ITP) of each order. Acceptance criteria are agreed with the client.
Inspection
- Stages
- Incoming, in-process and final inspection
- At receipt
- 100% check of documents and material, with traceability by material certificate and heat number
- ITP
- Hold, witness, review and spot points, signed off by our QC, third-party inspection and the client
- Dimensions
- Visual and dimensional checks; trial assembly of the first piece in a series
- Pressure test
- Hydrostatic tests of vessels and pipelines
- Final
- Final inspection report with DoP or DoC
- CE marking
- DoP for EN 1090 components
Non-destructive testing
- In-house
- VT and PT by our own staff, certified Level 2 by RINA Services
- Outsourced
- MT, RT and UT by accredited NDT laboratories
- Reports
- Issued in Bulgarian and English
Coating and surface
- Blasting
- Sa 2½, or Sa 3 where specified
- Chlorides
- Below 20 mg/m² before coating (C5 systems)
- Climate
- Temperature, humidity and dew point recorded at application
- DFT
- Measured per coat with calibrated electronic gauges; C5M system at least 240 µm
- Adhesion
- Pull-off or cross-cut tests
- Galvanizing
- Coating thickness checked
- Stainless
- Passivated and checked by copper sulphate test
Health, safety and environment
Risk assessments cover our workshop in Burgas and our project sites.
Safety rules and risk assessment
Our Occupational Health & Safety Policy Manual sets out responsibilities, training, risk assessments, first aid, PPE, fire safety and the rules on drugs and alcohol.
88 written safety instructions
They cover hot work, work at height, scaffolds, cranes and rigging, gas cylinders, chemicals, electrical work, excavation, winter work and PPE.
Incidents and near misses
Accidents and near misses are reported, registered and investigated. Each investigation records the root cause and the corrective actions.
Emergency plan and drills
We keep a written plan for disasters and accidents and hold practical drills. The drills are recorded.
Subcontractors
Subcontractors must have an HSE policy and system, provide health risk assessments and evidence of medical fitness, and accept our HSE audits.
Waste
Waste is segregated by stream. Scrap steel goes to recycling, oils and solvents are handled as hazardous waste, and we use licensed contractors.
Request a quotation
Send us your enquiry with all the necessary or available documentation. We reply in English, German and Bulgarian.